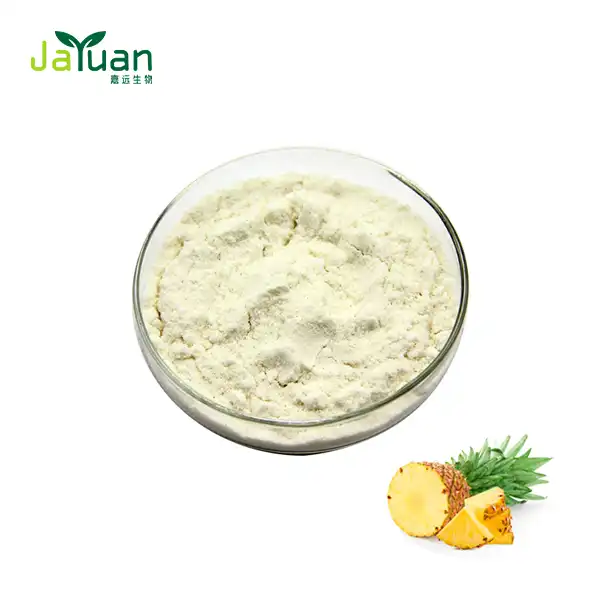
Bromelain Protein Enzyme Extract | High-Activity Plant-Based Proteolytic Solution for Food & Pharma Industries
Xi'an Jiayuan Bio-tech Co., Ltd., established in April 2002 with a registered capital of RMB 30 million, specializes in premium Bromelain Protein manufacturing. Our product offers standardised enzyme activity of 1000 GDU to 20,000 GDU/g and is manufactured in ISO9001 certified GMP manufacturing facilities.
The product is a thiol endopeptidase complex from pineapple stems with higher efficiency of protein degradation at pH 4.5-9.5. We deliver reliable, non-animal derived proteolytic solutions optimised for industrial scale applications in meat processing, nutraceutical formulation and clinical recovery procedures. Backed by a team of 30 skilled scientific professionals with more than 20 years of extraction experience.

What Is Bromelain Protein?
It is a combination of sulfhydryl proteolytic enzymes derived from the stems of the pineapple plant (Ananas comosus). It catalyses the hydrolysis of peptide bonds, leading to the breakdown of proteins into amino acids and smaller peptides.
This bioactive enzyme system consists of units of endopeptidases, phosphatase, glucosidase and peroxidase. It is also stable across a broad pH range unlike animal-derived enzymes such as pepsin or trypsin, addressing key issues in vegan-friendly formulations.
The optimum temperature and pH of this glycoprotein (molecular weight 24.5–27 kDa) are 50°C–60°C and pH 6.0–8.0, respectively. It preferentially hydrolyzes myofibrillar proteins . The peculiar substrate specificity fits the industrial needs for efficient improvement of protein digestibility and inflammatory control in medicinal applications.
COA
| Product Name | Bromelain Protein | ||||
| Lot No | 240414 | Quantity | 130kg | ||
| Manufacture Date | 2024.05.15 | Expiry Date | 2026.05.14 | ||
| Extract Source | Pineapple stem | Origin | China | ||
| Ref standard | According with the enterprise standard | ||||
| Items | Requirements | Results | Method | ||
| Appearance | Off-white or light yellow powder | Conforms | Visual | ||
| Odor | Characteristic | Characteristic | Organoleptic | ||
| Loss on drying | ≤10.0g/100g | 6.11g/100g | USP39<731> | ||
| Bromelain activity | ≥1800 GDU/g | 1850 GDU/g | GDU method | ||
| Residue of ignition | 6.0g/100g | 3.2g/100g | USP39<281> | ||
| Lead(Pb) | ≤5.0mg/kg | Conforms | USP39<233>ICP-MS | ||
| Cadmium(Cd) | ≤1.0mg/kg | Conforms | USP39<233>ICP-MS | ||
| Mercury(Hg) | ≤3.0mg/kg | Conforms | USP39<233>ICP-MS | ||
| Arsenic (As) | ≤1.5mg/kg | Conforms | USP39<233>ICP-MS | ||
| Total Plate Count | ≤10000cfu/g | 40cfu/g | USP39<61> | ||
| Mold &Yeast | ≤100 cfu/g | 10cfu/g | USP39<61> | ||
| E. Coli | Negative | Not Detected | USP39<62> | ||
| Salmonella species | Non-detected | Not Detected | USP39<62> | ||
| Staphylococcus aureus | Non-detected | Not Detected | USP39<62> | ||
| Storage conditions | Sealed and store in cool and dry place.For long time storage,please seal and store at/below 5℃ to keep the enzyme activity | ||||
| Conclusion | The product conforms to the enterprise standard | ||||
Functions
This enzyme's proteolytic capacity provides many functional benefits:
Protein Digestion Support: Boosts the digestion of complex protein structures into accessible amino acids. This increases efficiency of absorption of nutrients in digestive supplement formulations.
Anti-inflammatory Action: Modulates the arachidonic acid cascade to reduce oedema and post-operative swelling. Clinical investigations have shown it reduces systemic inflammation without the adverse effects of NSAIDs.
Collagen Hydrolysis: Works on connective tissue proteins such as collagen and elastin. This feature makes it very helpful for therapeutic wound debridement and tissue healing.
pH Adaptability: Retains 70-85% action throughout gastric and intestinal pH ranges (1.5-8.5). Its higher stability compared to traditional proteases provides uniform activity across the whole digestive system.

Areas of Application
Food Processing & Meat Tenderising
Industrial meat processors use the enzyme to enhance the quality of lower-grade portions. Injected or used as a marinade component, it selectively breaks down collagen networks, without mushiness.
The enzyme is active in cold chain conditions and retains action at refrigeration temperatures. Controlled tenderising also improves consistency of texture and decreases ageing time in industrial beef production.
Digestive Health & Nutraceuticals
This component is used by formulation chemists in digestive enzyme blends designed for protein malabsorption. The dual pH stability enables operation at the same time in intestinal and stomach environments.
Typical uses are in post-meal digestive aids, sports nutrition recovery formulations and geriatric supplement lines needing improved protein bioavailability.
Pharmaceutical and Clinical Applications
An enzyme of high purity pharmaceutical grade is used in wound care products to remove burn eschar. Selective proteolysis speeds healing and does not damage good tissue.
Systemic enzyme treatment is used into post-surgical recovery programmes to minimise inflammation and promote tissue healing. The fibrinolytic nature of the enzyme helps to enhance circulation in regions of dysfunction.
Bakery & Dough Processing
In the automated biscuit making gluten hydrolysis treatments reduce the shrinking of the dough during baking. Controlled enzyme treatment decreases elasticity for consistent product dimensions and superior machinability on high speed manufacturing lines.

Quality Control
Our quality assurance protocol ensures consistent enzymatic performance:
|
Parameter |
Specification |
Test Method |
|
Enzyme Activity |
1000–20,000 GDU/g |
FCC Tyrosine Method |
|
Appearance |
White to Beige Powder |
Visual Inspection |
|
Moisture Content |
≤5.0% |
Loss on Drying |
|
Total Plate Count |
<10,000 CFU/g |
AOAC Method |
|
Salmonella |
Negative/25g |
ISO 6579 |
|
E. Coli |
Negative/10g |
ISO 16649 |
|
Lead (Pb) |
<3 ppm |
ICP-MS |
|
Arsenic (As) |
<2 ppm |
ICP-MS |
|
Mercury (Hg) |
<0.1 ppm |
ICP-MS |
Each production batch undergoes Gelatin Digestion Unit (GDU) assay verification. We provide detailed Certificates of Analysis documenting proteolytic activity curves and substrate breakdown kinetics.
Temperature-controlled extraction and spray-drying processes preserve enzymatic integrity. Our laboratory facilities conduct stability testing under accelerated aging conditions to guarantee 24-month shelf life when stored below 25°C.
Certificates
Our manufacturing facility holds comprehensive quality certifications:
ISO9001 Quality Management System (obtained 2012)
SGS Verification for manufacturing processes
HALAL Certification for religious dietary compliance
Private Science and Technology Enterprise of Shaanxi Province (recognized 2013)
High-tech Enterprise of Shaanxi Province certification
All Bromelain Protein batches meet FCC (Food Chemicals Codex) and USP (United States Pharmacopeia) standards for food and pharmaceutical applications.

Payment & Shipment
Payment Terms: For international transactions we offer T/T, L/C, Western Union and PayPal. We can work out flexible payment plans for existing partners.
Shipping Partners: We work with FedEx, DHL, EMS, UPS and TNT for fast worldwide delivery. We have worldwide airline and shipping partners for big orders.
Customs Support: We provide customs clearance support in Europe and the United States for customers unfamiliar with the import process. Door-to-door deliveries take the complexity out of logistics.
Lead Time: 3 business days to ship for samples. Usually, bulk manufacturing takes 15-20 days depending on the request quantities.
Pack and Ship
Packing: 25kg fibre drums with twin polyethylene liners for moisture protection. * Alternative packaging is available in 1kg, 5kg or as per requirements on request.
Storage Conditions: Store below 25°C. Store in a dry place. Keep bottle closed to avoid absorption of moisture and loss of action. Loss of activity is less than 5% per year under suitable storage conditions.
Transportation: Shipping in temperature-controlled containers preserves product integrity throughout transportation. For tropical route shipments of over 7 days, our logistics staff arranges for chilled containers.
After Sales Service
We provide full assistance after purchase:
Technical Consultation: Our R&D team will assist you with formulation advice and optimising enzyme dose rates for your unique applications.
Application Testing: Free sample supply (50-200g) to enable you to test performance in your production setting before a bulk commitment.
Quality Dispute Resolution: Any activity inconsistencies are resolved within 48 hours, with replacement or refund choices according to third-party testing.
Regulatory paperwork Support: We provide entire regulatory paperwork including CoA, Material Safety Data Sheets (MSDS) and allergy declarations to meet your compliance requirements.
Why choose us?
Direct from Manufacturer Pricing: We are factory direct, thus no middle man mark up. You get to save on your purchase prices with volume discounts and flexible MOQ rules.
Manufacturing Capability Established: The consistent supply is guarantyd by two GMP-standard manufacturing lines with more than 20 years of operation. Annual manufacturing capacity is more than 500 metric tons.
Customisation Options : Activity standardisation from 600 to 20,000 GDU/g We may adapt to certain enzymatic profiles that meet your technological needs.
Global Logistics Network: Warehousing partners in core markets facilitate consolidated shipment. Combining many items into a single package may save freight costs.
Quality Transparency: Each batch comes with complete enzymatic characterisation data. We track graphs of proteolytic activity over time in our CoA, to ensure substrate breakdown rates are predictable.

FAQ
Q: How does storage temperature affect the shelf life of the product?
A: The enzyme is temperature-sensitive and must be kept below 25°C and in dry circumstances. With these settings we still have activity loss below 5-10% on a yearly basis. High humidity or exposure over 40°C greatly increases deterioration.
Q: What is the difference between Stem Bromelain and Fruit Bromelain?
A: Stem Bromelain (EC 3.4.22.32) , the market benchmark, is present in our product. It has more abundant and cost-effective than Fruit Bromelain (EC 3.4.22.33). The enzyme from stem cells has varied proteolytic specificity optimised for commercial use .
Q: Can the product be used in baking applications?
A: Yes, it hydrolyzes the gluten in wheat and makes the dough less elastic. This feature is essential in automated biscuit manufacture, guaranteeing no shrinking and consistent dimensions in high speed processing lines.
Q: Is the product susceptible to inhibition by specific compounds?
A: As a thiol protease, it is inhibited by heavy metals (silver, mercury) and oxidizing agents. Heat treatment above 70-80°C causes irreversible inactivation—an important control point for stopping enzymatic reactions in finished food products.
Q: How is the 'bioactivity' of your product verified?
A: We utilize the FCC-standard Gelatin Digestion Unit (GDU) assay method. Each batch includes a Certificate of Analysis documenting specific proteolytic activity graphs against time, ensuring rapid and consistent substrate breakdown.
Contact Us
Ready to enhance your formulations with high-activity proteolytic Bromelain Protein solutions? Contact our technical sales team at sales@jayuanbio.com and sales1@jayuanbio.com for product specifications, pricing quotations, and free sample requests today.